Pallet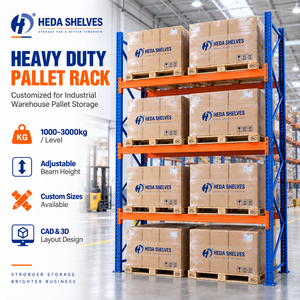
Heavy Duty Pallet Rack Industrial Storage System for High Load
100% selective access to every pallet with high load capacity — the workhorse choice for Charlestown distribution centres managing many SKUs.
View systemFrom pick-face carton flow to full-pallet high-bay storage, every system below is roll-formed and powder-coated on our own lines — then configured to your SKU profile, pallet weight and building height.
100% selective access to every pallet with high load capacity — the workhorse choice for Charlestown distribution centres managing many SKUs.
View system
A modular, bolt-together frame that grows with your throughput — ideal when a facility adds bays phase by phase without stopping operations.
View system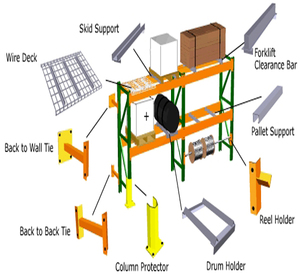
Boltless assembly plus phosphated, powder-coated steel for coastal humidity and cold-chain rooms where rust attacks unprotected frames.
View system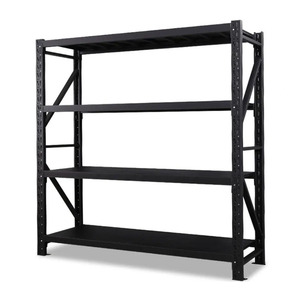
Cold-rolled steel shelves rated around 200 kg per level, adjustable in height — for spare parts, pharmacy stock and retail backrooms.
View system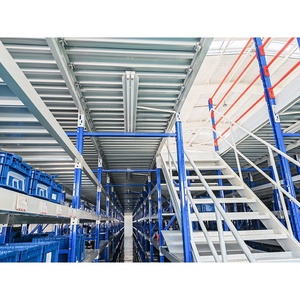
Multi-tier steel platforms that double usable floor area without new construction — proven in e-commerce and chemical plant warehouses.
View system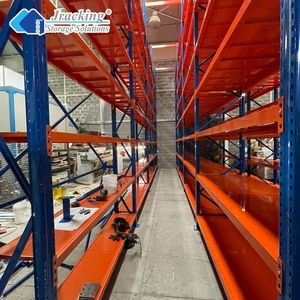
European-profile beams and uprights sized for fast-moving distribution operations that need predictable load charts and quick bay reconfiguration.
View system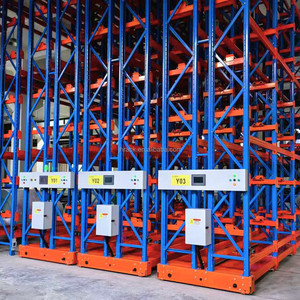
Racks that roll on floor tracks to open a single aisle on demand — typically recovering 40–50% of floor space in high-rent urban warehouses.
View system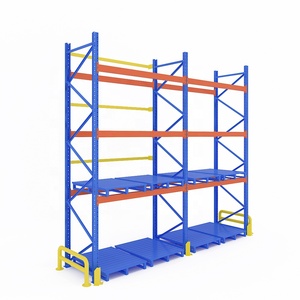
Integrated back stops prevent pallets from pushing through to the next aisle — a simple, low-cost upgrade that reduces product damage and claims.
View system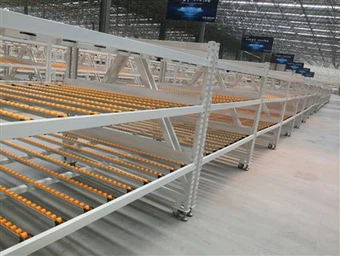
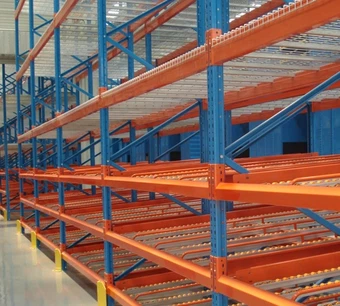
Carton flow (also sold as gravity flow or flow rack) is not simply shelving on an incline. It is a FIFO-controlled pick module: cartons load at the back, roll forward on inclined roller or skate-wheel tracks, and present automatically at the front pick face. The picker never walks into a lane, never reaches over stock, and never restocks from the picking side.
For a Charlestown operation mixing high-SKU-count picking with a constrained floor plate, that translates into measurable economics. Industry planning benchmarks commonly cite productivity gains of 30–50% on carton picking versus static shelving, and floor-space savings of 40–60% versus conventional selective racking at the same pick-face count — because lanes can be stacked with tighter vertical pitch.
The right system depends on what moves through the building — not on a catalogue page. These are the configurations we specify most often for the Charlestown market.
Carton flow pick modules and light-duty shelving for high-SKU fulfilment, with mezzanine decks where pick density beats storage density.
Boltless corrosion-protected frames and carton flow lanes in chilled rooms, where every second pickers spend inside the freezer costs money.
Light-duty adjustable shelving for components plus heavy-duty pallet rack for raw material — one supplier, one consistent load chart.
High-bay pallet rack and mobile systems for pallet-volume rotation, with back stops to prevent push-through damage in fast lanes.
Storage decisions made five years ago no longer match today's order profile. Three trends sit behind almost every layout brief we receive from the Charlestown market right now.
Because we manufacture carton flow, pallet rack, mezzanine and mobile systems under one roof, we can propose a hybrid layout rather than force-fitting a single product family to the whole building.
These are the four data points that change a racking design most — and the four most commonly missing from first enquiry emails.
Length, width, height and weight per carton set lane width, roller pitch and the number of flow levels per bay. A 10 mm difference can change the bay count.
Usable clear height minus sprinkler clearance and roof trusses determines maximum tier count — the single biggest factor in cost per storage position.
Concrete thickness and strength govern upright point loads and anchor specification. On mezzanines, it governs whether columns can land where the layout needs them.
Site seismic classification and local code requirements drive bracing, base plates, row spacers and chemical anchors — always confirmed with a locally licensed engineer.
Coastal air, tropical humidity and freezer cycling all accelerate corrosion. We specify hot-dip galvanized or pre-galvanized components where standard powder coat is not enough.
Forklift type, lift height and aisle turning radius fix the aisle width — which in turn fixes how much storage you actually get per square metre.
Lottot Storage Solutions has designed and manufactured industrial storage systems in its own facility since 2007 — so the engineer who calculates your load capacity is part of the team that builds and ships it.
CE and ISO certified materials, controlled roll-forming tolerances and quality recognised by clients in more than 60 countries.
Free consultation with professional engineers, free warehouse layout design and an optimised storage solution for your operation.
Factory-direct supply with no trading layers, and transparent, itemised quotations for distributors and project contractors.
20+ automatic roll-forming lines and 30,000 tons of annual output secure production in 10–15 days after drawing approval.
10-Year Warranty. All racking products are covered for ten years against quality issues caused by our design, manufacturing, transportation or installation guidance — plus 2D/3D layout and itemised quotation within 48 hours.
Yes. We supply carton flow racking, selective and heavy-duty pallet racking, mezzanine platforms, mobile racking and light-duty shelving to the Charlestown market under FOB, CFR or CIF terms, with DDP available on request. Full-container and consolidated loads are both supported, and we prepare commercial invoice, packing list, bill of lading and certificate of origin for each shipment.
Send your warehouse plan (CAD or PDF), carton and pallet dimensions, weights and clear height, and our engineers return a 2D/3D layout with load calculations and an itemised quotation within 48 hours. Standard production then runs 10–15 days after drawing approval.
Yes. We calculate upright, beam and anchor requirements against the seismic zone, soil class and floor slab data for your site, and typically specify reinforced base plates, heavier bracing, row spacers and chemical anchors. We always recommend final validation by a locally licensed structural engineer before installation.
Standard components receive phosphating pre-treatment followed by electrostatic powder coating. For coastal, high-humidity or freezer environments we offer hot-dip galvanized and pre-galvanized components, which substantially extend corrosion resistance where standard coating is not sufficient.
All racking products carry a 10-year warranty against quality issues arising from our design, manufacturing, transportation or installation guidance. Routine inspection of racking in service is still recommended, as impact damage from handling equipment is the most common cause of rack failure in any warehouse.
Yes — and it is usually the better answer. A typical Charlestown layout combines carton flow pick modules at the pick face, selective or high-bay pallet rack for reserve storage, and a mezzanine where pick density is the constraint. Because all of these are manufactured in our own facility, they are quoted as one integrated system with a consistent load chart and colour finish.
Send us your floor plan, carton and pallet data, and clear height. Our engineers will return a free layout, load calculation and itemised quotation within 48 hours.
Inquire Now